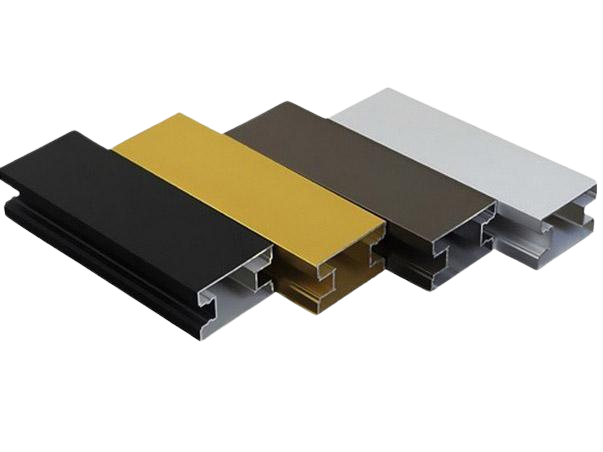
PVDF Coated Aluminum Profiles
What is PVDF for Extruded Profiles?
PVDF (polyvinylidene fluoride) is a fluoropolymer coating system applied to extruded aluminum profiles via multi-coat spray and high-temperature bake. Using architectural-grade PVDF resin (typically 70% fluoropolymer per Kynar 500/Hylar 5000 specifications), it forms a dense, UV-stable, and corrosion-resistant finish tailored to complex profile geometries.

Advantages of PVDF Coated Aluminum Extrusions
Exceptional weatherability (20–30+ years): PVDF maintains color and gloss under strong UV, rain, salt spray, and thermal cycling, making it ideal for façades and exposed frames; proven field performance in coastal and desert climates shows low chalking and minimal gloss loss, supporting long warranties and extending repaint cycles.
Superior corrosion protection: The dense fluoropolymer barrier blocks moisture, chlorides, and industrial pollutants, and when paired with proper conversion coating and primer it resists underfilm corrosion at edges and joints; this is especially valuable for hollow and intricate extrusions where crevices can trap contaminants over time.
Outstanding color and fade resistance: Strong C–F bonds and UV-stable pigments deliver ultra-low chalking and minimal ΔE, even for dark, saturated, or metallic/mica colors, ensuring consistent appearance across orientations and elevations; this reduces replacements due to mismatch and preserves the original design intent.
Low dirt pickup and easy cleaning: The low-surface-energy finish sheds dust, soot, and grime, so routine rinsing with water and neutral detergent typically restores appearance; in polluted urban or coastal zones, reduced soiling and easier maintenance mean fewer cleaning cycles and lower access costs.
Flexibility and durability on complex profiles: PVDF retains flexibility after cure to accommodate expansion and contraction of long, thin-wall extrusions without cracking at corners or sharp radii, and it shows good mar/abrasion resistance during fabrication and installation when properly cured, reducing rework and touch-up on site.
PVDF Coating Process
Pretreatment for complex sections: alkaline degrease → rinse → conversion coating (chromate or chromate-free) → dry; special attention to hollows/voids and drainage to avoid residue.
Primer: epoxy or polyester primer to boost adhesion and edge corrosion resistance.
PVDF topcoat: controlled spray angles/racking to cover deep channels, sharp edges, and backwalls.
Optional clearcoat: increases abrasion resistance and fine-tunes gloss/self-cleaning.
Cure: typically around 200°C with time/temperature verified on heavy/thin sections to avoid under- or over-bake.
QA for profiles: film thickness mapping on edges, corners, recesses; cross-hatch adhesion, MEK rubs, gloss and color ΔE checks.
PVDF coating Film Further
Total DFT: 25–35 μm typical; 35–45 μm for severe exterior exposure.
Corner/thin-wall coverage: optimize gun setup and line speed to avoid thin spots and runs on sharp radii and narrow webs.
Appearance: matte/semi-gloss/high-gloss; metallic/mica orientations controlled for uniform look across long profiles.
Comparison with Other Surface Finishes
| Item | PVDF Coating | Anodizing | Polyester Powder | Electrophoretic Coating (E-coat) |
|---|---|---|---|---|
| Outdoor durability | Excellent, 20–30+ years | Very good; dyed colors may fade | Good, below PVDF in high UV | Moderate; best indoors |
| UV/fade resistance | Excellent | Natural anodize good; dyed average | Medium to good | Limited |
| Corrosion resistance | Excellent (with pretreatment + primer) | Very good; needs good sealing in marine | Good | Good; needs topcoat for harsh exterior |
| Cleaning/soiling | Low dirt pickup, easy to clean | Hard surface, can stain | Average | Very smooth; easy indoors |
| Mechanics/edge coverage | Flexible; resists corner cracking | Hard; damage is visible | Thick film; great edge coverage | Thin, very smooth |
| Appearance options | Widest color/gloss range | Strong metallic look; limited colors | Many colors; textures possible | Very smooth; fewer colors |
| Batch consistency | High (manage metallic orientation) | Sensitive to alloy/process | High | High |
| Complex profiles | Good; needs spray angle/racking control | Inner cavities not treated | Very good | Very good (coats internals) |
| Film thickness | 25–35 μm | 10–20 μm | 60–120 μm | 10–25 μm |
| Initial cost | High | Medium–high | Low–medium | Medium |
| Lifecycle cost | Low | Medium | Medium to higher (exterior) | Medium–high (exterior) |
| Best use cases | Coastal/high-UV façades, long warranties | Metallic look, abrasion-resistant parts | Cost-effective façades, inland | Interior parts, complex hollows |
About HTS-ALU
HTS New Materials (Jiangxi, China) is a leading aluminum extrusion manufacturer with 40+ advanced lines and presses up to 6,000 tons. We supply profiles for construction, industrial uses, and premium doors/windows, including thermal-break profiles.
Capabilities include anodizing, powder coating, fluorocarbon coating, and wood-grain transfer. We also offer end-to-end machining and fabrication: CNC, milling, punching, drilling, threading, precision cutting, welding, and assembly—delivering ready-to-use, project-specific solutions.
Hot-Selling Products
Custom Extrusion Steps
- Share your CAD/STEP files or a physical sample.
- We create manufacturing drawings.
- You review and approve the drawings.
- We manufacture the extrusion die.
- We run a trial extrusion.
- You validate and sign off the samples.
- We begin mass production.
- Typical extrusion lead time is about 15 days.
- Extra time is added for finishing or machining.
- We perform in-process inspections.
- We conduct final inspections before shipment.
- We protect each profile to prevent abrasion.
- We pack per your requirements.
- We arrange shipment by sea, air, rail, or multimodal.
Alloys for Extruded Profiles
- 6063 (T5/T6)
- 6061 (T6/T6511)
- 6060 (T5)
- 6005/6005A (T5/T6)
- 6082 (T6)
- 6101 (T6/T61)
- 7075 (T6/T73)
- 2024 (T351)
Aluminum Profile Weight per Meter
Formula: W(kg/m) = A(mm²) × 0.00272 or A(cm²) × 0.272
Packing Options
- Single-piece protective film separation
- Blister packaging
- Carton packaging
- Wooden crate packaging
- Palletization