Bespoke Aluminium Profile Extrusion
Bespoke aluminium profile extrusion is the process of forcing aluminium billets through a precision die to produce continuous profiles with a defined cross‑section. Each distinct cross‑section requires its own die; while generic profiles—round tube, square tube, U‑channel, L‑angle, and T‑slot—are commonly stocked, many applications demand purpose‑built tooling to achieve exact geometry, tolerances, and integration features. Beyond shape, the selection of alloy and temper (heat treatment) governs strength, formability, corrosion resistance, and weldability, while surface finishes such as anodizing, powder coating, and electrophoresis determine appearance and durability.
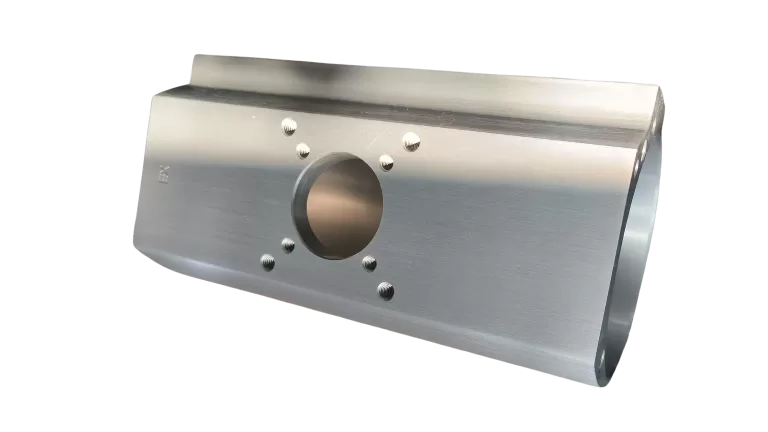
Post‑extrusion operations further expand functionality and precision. CNC machining (milling, drilling, tapping, slotting), cutting, straightening, and forming can be applied after extrusion to meet assembly and performance requirements. This article will define the key decision points for bespoke aluminium profile extrusions, clarify trade‑offs among geometry, material, temper, and finish, and conclude with an overview of HTS‑ALU’s bespoke extrusion and value‑added manufacturing capabilities.

Drawings or Samples for Bespoke Aluminium Profiles
Providing a complete cross‑section drawing is essential for bespoke aluminium profile extrusion. Please submit a clear CAD drawing (DXF/DWG) of the cross‑section to enable feasibility assessment, optimization recommendations, and rapid quotation. If post‑extrusion machining is required, also include a 3D model in STEP format to clarify features such as holes, slots, counterbores, threads, datum schemes, and assembly interfaces.
From sample to drawing: We can reverse‑engineer from a physical sample. With advanced profile scanning equipment, we generate the technical drawing and return it for your confirmation before tooling.
Tolerance specification: Explicit tolerances are necessary for manufacturing and quality control. Wherever possible, indicate dimensional tolerances, geometric tolerances (e.g., flatness, straightness, perpendicularity), and surface finish requirements directly on the drawing.
Supplementary details: Include alloy and temper, surface treatment, nominal length, cut length tolerances, straightness/camber limits, and any critical-to-quality dimensions.
By standardizing deliverables in CAD and STEP formats and embedding tolerances in the documentation, we accelerate DFM review, reduce ambiguity, and ensure accurate, timely quotations.
Material Options for Bespoke Aluminium Profiles
Selecting the right alloy is fundamental to performance, cost, and finish quality. Extrusions commonly use 6xxx series alloys due to their good extrudability and anodizing response, with 6063 being the mainstream choice. Depending on application requirements—strength, corrosion resistance, machinability, or finishing—other alloys may be preferable. Below are widely used options:
6063: The most common extrusion alloy for general applications (e.g., architectural doors/windows, heat sinks). Excellent surface finish and anodizing response; suitable for fine details and thin walls.
6060: Very similar to 6063 and frequently used in Europe. Good extrudability and surface finish, typically for architectural and decorative profiles.
6061: Higher strength than 6063 with slightly inferior anodized appearance. Favoured for mechanical frames, fixtures, and structural components where rigidity matters.
6082: Offers higher strength than 6061 in many tempers and better fatigue performance; used for load‑bearing parts and heavier duty frameworks.
7075: Among the highest‑strength aluminium alloys; used in aerospace and defence where strength‑to‑weight is critical. Limited corrosion resistance relative to 5xxx/6xxx and more demanding to extrude; finishing options are more constrained.
2024: High strength, second to 7075 in many tempers, with excellent fatigue resistance. Common in aerospace components; corrosion protection measures are typically required.
5083: Non‑heat‑treatable, outstanding corrosion resistance—ideal for marine environments and chemical exposure. Moderate strength; welding performance is excellent.
Heat Treatment Options for Bespoke Aluminium Profiles
Heat treatment tailors mechanical properties, dimensional stability, and downstream processing behavior. For aluminium extrusions, the most common tempers are T5 and T6, with additional options for specific performance targets.
T5: Air cooling after extrusion followed by artificial aging.
- Characteristics: Balanced strength and stability; shorter cycle time; good for profiles requiring decent machinability and good anodizing response.
- Use cases: Architectural profiles, general‑purpose frameworks.
T6: Rapid quench (typically water quench) after extrusion, then artificial aging.
- Characteristics: Higher strength than T5; may increase residual stresses and distortion risk during machining; sometimes requires stress‑relief strategies.
- Use cases: Structural members, precision mechanical components demanding higher strength.
T66: Quench, straightening, then artificial aging.
- Characteristics: Strength level comparable to or slightly above T6 for certain 6xxx alloys, with improved dimensional control due to straightening.
- Use cases: Long, slender profiles where straightness and tight tolerances are critical.
T73: Quench followed by two‑stage artificial aging.
- Characteristics: Lower peak strength than T6 but enhanced stress‑corrosion cracking resistance; improved reliability in harsh environments.
- Use cases: Components exposed to corrosive or cyclic environments, particularly in transportation and marine applications.
Surface Finishing Options for Bespoke Aluminium Profiles
Selecting the right surface treatment affects corrosion resistance, appearance, electrical properties, and durability. Below are common finishing options for aluminium extrusions, from untreated to highly decorative or functional coatings.
Mill finish: As‑extruded surface without additional treatment. Aluminium naturally forms a thin, dense oxide layer in ambient air, which inhibits further corrosion—unlike ferrous metals. Mill‑finish profiles are acceptable for many applications, especially indoor or low‑exposure environments.
Anodizing (clear or dyed): An electrolytic process that grows a uniform, controlled oxide layer on the surface.
- Benefits: High hardness, improved wear and corrosion resistance, excellent adhesion base for dyes, and electrically non‑conductive surface.
- Options: Clear (natural) anodizing; dyed/anodic coloring in black, bronze, champagne, and custom hues; hard anodizing for elevated wear resistance.
Electrophoretic coating (E‑coat over anodized base): Typically applied after anodizing to enhance color depth and gloss.
- Benefits: High color consistency, refined gloss, improved corrosion resistance, and good UV stability for architectural applications.
Powder coating: Thermoset or thermoplastic powders applied electrostatically and cured.
- Benefits: Robust, uniform coating with excellent corrosion and scratch resistance.
- Color options: Full RAL palette, custom colors, textures, and finishes; selectable gloss levels from high‑gloss to matte.
Wood‑grain transfer (sublimation): Decorative finish that transfers a wood pattern onto a pre‑coated (often powder‑coated) base.
- Benefits: Realistic wood appearance with the durability of metal; suitable for doors, windows, and architectural trims.
Other metallic or protective platings/coatings:
- Examples include tin plating, nickel plating, or conversion coatings where specific electrical or barrier properties are required. Note that traditional electroplating on aluminium typically requires special pretreatment and an intermediate layer.
Texture and pre‑treat options:
- Sandblasting/shot blasting: Creates a uniform matte texture, improves coating adhesion.
- Brushing: Linear grain for a satin metallic look; often combined with clear anodizing.
- Polishing/mirror finish: High reflectivity; usually followed by clear anodizing or lacquer to preserve gloss.
- Chemical conversion (chromate‑free alternatives): Enhances paint adhesion and provides baseline corrosion protection, often as a pre‑paint step.
Machining and Value‑Added Operations for Bespoke Aluminium Profiles
Bespoke aluminium profiles often require secondary processing to meet functional and assembly requirements. Aluminium offers excellent machinability, enabling precise, efficient, and cost‑effective value‑added operations.
Cutting and general subtractive machining:
- Sawing and precision cutting: Straight, miter, and compound cuts; length tolerances and burr control specified per drawing.
- CNC milling/drilling/tapping/slotting: Creation of pockets, keyways, counterbores, threads, and complex features; fixturing strategies minimize distortion on thin‑wall sections.
- Deburring and edge finishing: Mechanical or thermal deburring to ensure safe handling and consistent assembly fit.
Forming and fabrication:
- Bending and forming: Rotary‑draw bending, roll forming, and stretch forming for curved profiles; springback compensation based on alloy and temper.
- Welding: TIG/MIG welding for 5xxx/6xxx alloys; filler selection and heat input control to preserve mechanical properties and surface finish.
- Riveting and fastening: Installation of threaded inserts, clinch nuts, and custom hardware.
Assembly services:
- Telescopic assemblies: Nested round or square tubes with bushings, detents, or locking mechanisms for smooth extension.
- Frame and module assembly: T‑slot frameworks, hinges, end‑caps, seals, and gasketing; functional testing and kitting available.
Marking and identification:
- Laser engraving/marking: High‑contrast, durable marks for logos, serial numbers, and traceability; compatible with anodized surfaces.
- Silk‑screen printing (pad/screen): Color graphics and instructions; RAL/Pantone color matching and abrasion‑resistant inks.
- Dot‑peen and inkjet coding: Industrial traceability on high‑volume runs.
Quality and process controls:
- GD&T conformance: Hole positions, parallelism, flatness, and straightness verified with CMM/optical metrology.
- Stress and distortion management: Sequence planning, step‑clamping, and rough‑then‑finish machining for T6/T66 tempers.
- Surface integrity: Protect cosmetic faces with films and fixtures; define acceptable cosmetic grades.
Specify machining features on the STEP model and 2D drawings (.STEP + .DWG/.DXF), including tolerances, datum schemes, and finish requirements. Clear documentation accelerates DFM review, reduces rework, and ensures repeatable production quality.
Packaging Options for Bespoke Aluminium Profiles
Proper packaging safeguards cosmetic surfaces, preserves dimensional integrity, and streamlines handling from factory to site. Select options based on profile geometry, surface finish, shipping mode, and handling frequency.
Surface wrapping
- Shrink‑wrap/bubble film bundles: Multiple straight, regular‑shaped profiles can be wrapped together with vacuum or shrink film when mutual abrasion risk is low. This is efficient for transport and reduces packing time.
- Foam paper single‑piece wrap: Irregular or highly profiled surfaces, sharp ribs, or high‑gloss/ anodized finishes should be wrapped individually with foam paper (or foam sleeve) to prevent scuffing and denting.
- Protection notes: Add corner guards for sharp edges; use interleaves between anodized/powder‑coated parts to avoid rubbing.
Container loading (loose loading)
- Common for architectural door/window profiles. Bundled profiles are loaded directly into containers to maximize volume utilization. Ensure spacers and blocking are used to control movement and avoid compression damage near the container doors.
Palletization
- Profiles are bundled, strapped, and stacked on fumigated wooden or plastic pallets, then stretch‑wrapped.
- Benefits: Forklift‑friendly, faster cross‑docking, better stackability, and improved protection against floor moisture.
- Options: Edge protectors, anti‑slip layers, and top‑boards to distribute strap pressure.
Crating (wooden cases)
- Robust wooden crates for mixed or long‑haul shipments, especially in LCL/consolidated containers.
- Benefits: Superior impact protection, controlled stacking, and ease of customs inspection. Specify maximum crate weight and dimensions per route limits.
Carton boxes
- Suitable for decorative trim, smaller mouldings, and retail kits. Parts are individually wrapped or sleeved, then packed in labeled cartons with inner partitions. Cartons can be palletized for bulk shipment.
Labeling and documentation
- Include part number, PO, alloy/temper, finish, length, quantity, and handling symbols on each bundle/carton.
- Apply barcodes or QR codes for traceability; indicate orientation or “Do Not Stack” where relevant.
Export and compliance options
- ISPM‑15 compliant wood for international shipments; moisture control with desiccants and VCI as needed.
- Drop, vibration, and compression testing can be performed for validated packaging specs on high‑value or cosmetic‑critical profiles.
Match packaging to geometry and finish—bundle regular, robust profiles together; individually wrap irregular or premium‑finish parts; choose pallets or crates according to shipping mode and handling requirements.
Pricing for Bespoke Aluminium Profiles
The cost of bespoke aluminium profile extrusion is a combination of several factors. Understanding each component helps with budgeting, design trade‑offs, and quotation accuracy.
Tooling (die) cost
- Larger or more complex cross‑sections require stronger, multi‑cavity or bridge dies, increasing cost and lead time. Tight tolerances and thin walls can also raise tooling complexity.
Aluminium ingot price
- The metal cost tracks local exchange/market quotations and is relatively consistent within a region. Price fluctuations directly affect piece price, especially for high‑mass profiles.
- Bigger cross‑sections demand higher‑tonnage presses and slower run speeds, increasing cost. Hollow or deep‑ribbed shapes may require porthole dies and additional process control.
Heat treatment cost
- Pricing varies by temper: T6 typically costs more than T5 due to quenching logistics and longer aging cycles. Tempers like T66/T73 may add straightening or multi‑stage aging steps.
Surface finishing cost
- Depends on process and specification: basic clear anodizing < dyed anodizing/E‑coat < powder coating < specialty finishes (hard anodize, wood‑grain transfer). Thickness, color consistency, and standards compliance (e.g., Qualanod/AAMA) also influence price.
Machining and fabrication cost
Driven by feature complexity, tolerances, cycle time, and fixturing needs. Operations include cutting, CNC milling/drilling/tapping, bending, welding, assembly, and marking.
Important sequencing note:
- Doing surface finishing first and then machining will break the coating at machined areas and may require rework or local touch‑up.
- Machining before finishing preserves coating integrity but increases finishing labor (masking, racking, handling). Choose the sequence based on cosmetic and functional priorities.
Packaging cost
- Varies with protection level: multi‑piece shrink‑wrap bundles are economical; individual foam wrapping, palletization, cartons, or wooden crates increase material and labor costs, but reduce transit damage risk.
Other cost drivers (recommend specifying on RFQ)
- Target volume and batch size (affects amortization of setup and tooling)
- Lengths and cut tolerances; scrap rate assumptions
- Alloy and temper availability; lead‑time constraints
- Quality requirements (CMM reports, PPAP, certificates, coating thickness tests)
Tailored Aluminium Profile Solutions
HTS‑ALU delivers end‑to‑end, vertically integrated services for bespoke aluminium profiles—from alloy casting to precision machining and export‑ready packaging—enabling tight control over quality, lead time, and cost.
Alloy customization
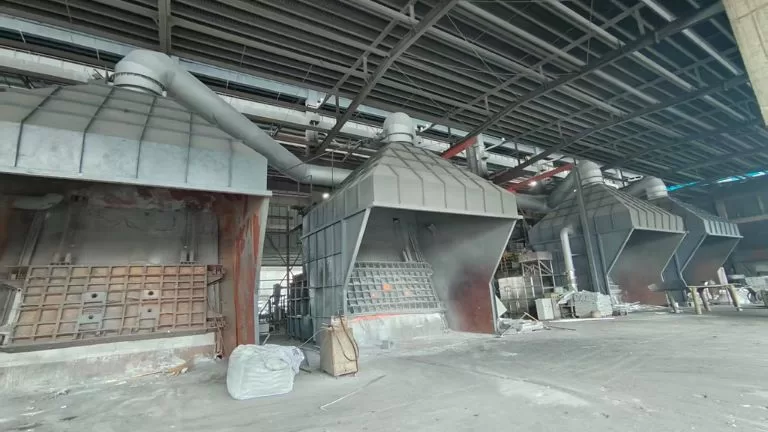
- In‑house billet casting supported by 4 melting furnaces allows tailored chemistries and temper planning to match strength, corrosion resistance, extrudability, and finishing requirements.
Extrusion capacity
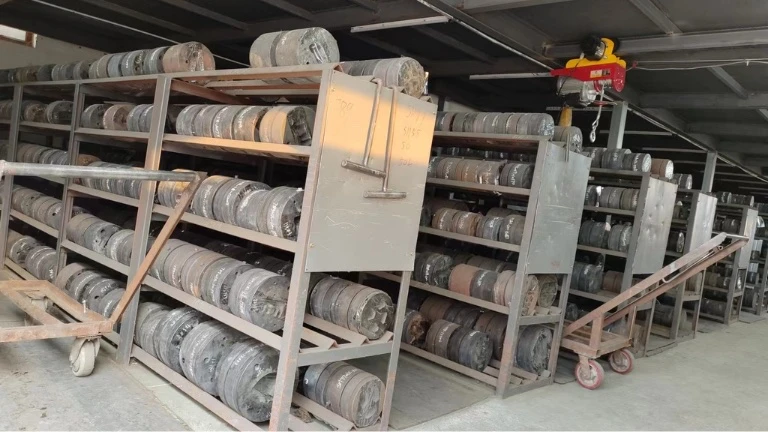
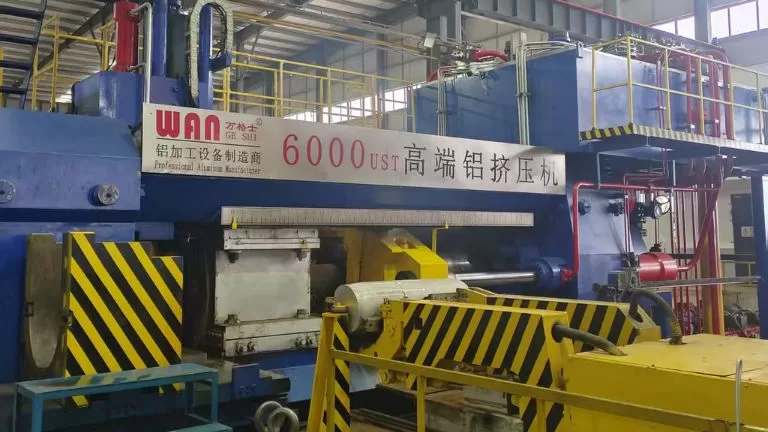
- 40 extrusion presses covering a wide tonnage range, including reverse (backward) extrusion for seamless tubes.
- Maximum press capacity: 6,000‑ton, enabling large cross‑sections, deep hollows, and heavy‑duty structural profiles with stable throughput.
Heat treatment
- Water quench capability for high‑strength tempers and distortion control.
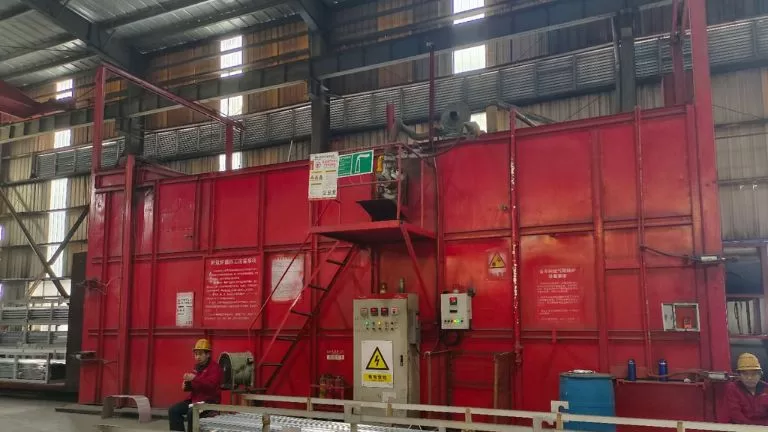
- Aging ovens accommodating lengths up to 8 meters, supporting T5/T6/T66/T73 and customized stress‑relief schedules.
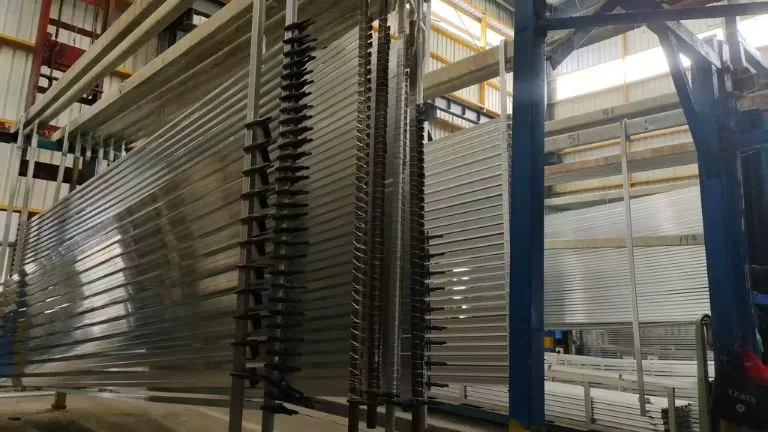
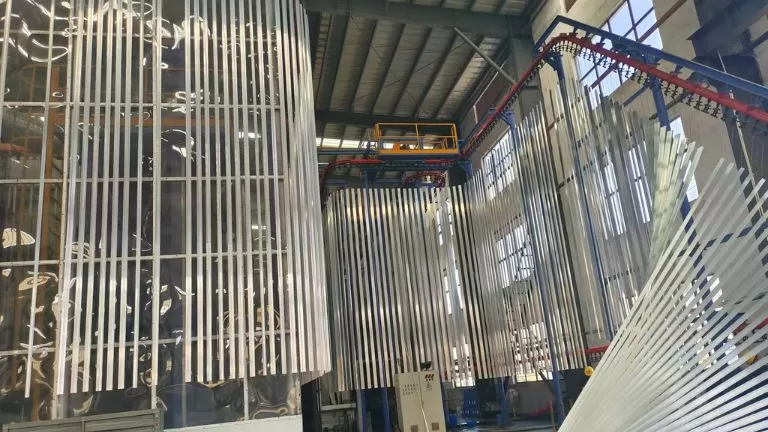
- Comprehensive finishes: clear and colored anodizing, hard anodizing, electrophoretic coating, vertical and horizontal powder coating lines, PVDF coating, wood‑grain transfer, sandblasting, brushing, and mirror polishing.
- Process control aligned to architectural and industrial standards for consistent color, gloss, and film thickness.
Precision machining
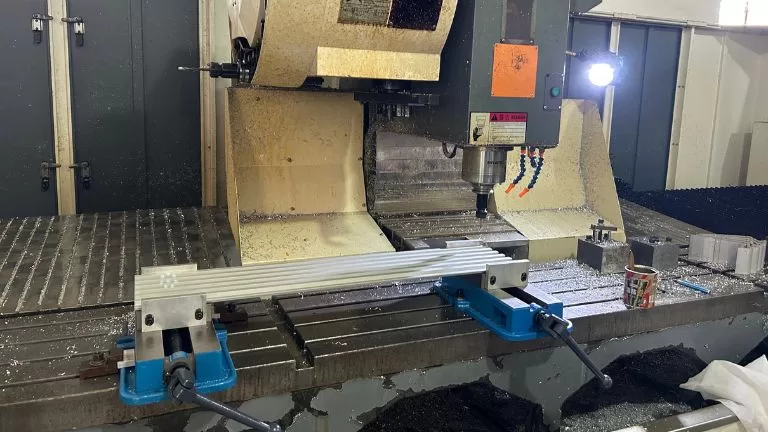
- 5‑axis CNC machining centers capable of processing profiles up to 6 meters in a single setup.
- Full suite of drilling, tapping, milling, slotting, welding, and assembly services, plus laser marking and silk‑screen printing for identification and branding.
Packaging to specification
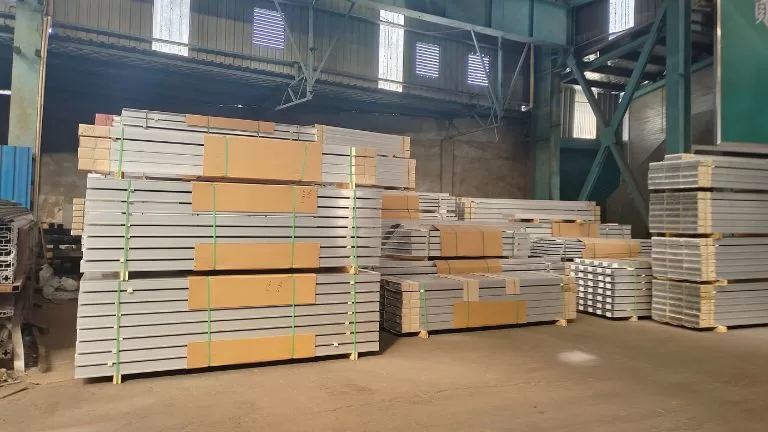
- Custom packaging solutions including multi‑piece shrink‑wrapped bundles, individual foam wraps, palletization, wooden crating, and retail cartons—engineered to minimize transit damage and meet ISPM‑15/export requirements.
HTS‑ALU provides a one‑stop aluminium profile solution: fully integrated in‑house capabilities from alloy casting to finishing and machining, and for any process not available internally, we coordinate trusted subcontracting to deliver the complete specification.