Aluminum Extrusion Manufacturing
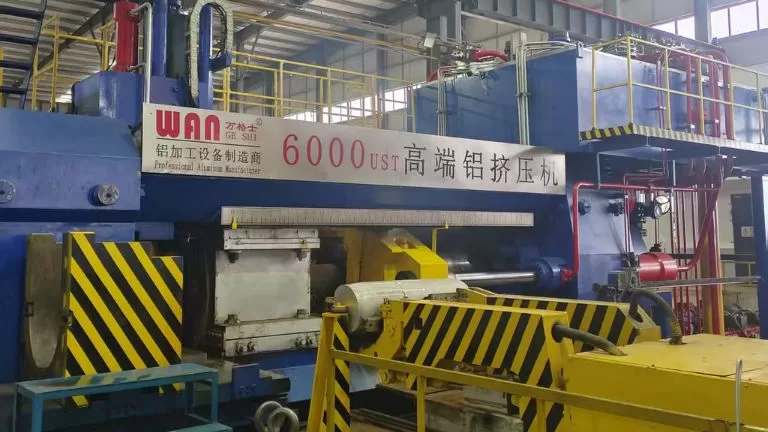
High-Capacity Production Scale: 40 advanced extrusion lines ensure rapid throughput, flexible scheduling, and stable supply for both high-volume and multi-spec orders.
Heavy-Duty Extrusion Capability: Equipped with presses up to 6,000 tons, enabling large profiles, complex cross-sections, thick-wall parts, and high-strength alloys with excellent dimensional stability.
Custom Die Design & Development: In-house mold engineering and rapid tooling iteration deliver optimized flow balance, reduced die trials, tighter tolerances, and faster time-to-market for bespoke profiles.
End-to-End Heat Treatment: Integrated solution covering aging, quenching, and temper control for alloys such as 6xxx and 7xxx, achieving target tempers (e.g., T5/T6), enhanced mechanical properties, and consistent performance.
Advantages of Aluminum Extrusion Manufacturing
Aluminum extrusion is a highly efficient manufacturing process that produces continuous profiles by forcing heated aluminum billets through a precision die. It is widely used for construction, transportation, industrial equipment, electronics, and furniture applications.
Compared with many metal forming processes, aluminum extrusion offers excellent material utilization, lower tooling costs, and high production efficiency. It is particularly suitable for producing long parts, complex cross-sections, and large-volume production runs.
Although extrusion creates constant cross-sectional shapes, it can be combined with CNC machining, drilling, tapping, welding, and assembly processes to manufacture complex finished components and engineered systems.
Types of Profiles Produced by Aluminum Extrusion
Aluminum extrusion can produce a wide variety of profile shapes, making it one of the most flexible manufacturing methods for aluminum components. Depending on structural and functional requirements, profiles can be designed as solid sections, hollow sections, or multi-cavity profiles.
In addition to closed shapes, aluminum extrusion also supports open-profile designs such as channels, angles, T-sections, and custom functional profiles. These designs are widely used in windows and doors, industrial equipment, furniture, transportation systems, and electronic products.
Aluminum extrusion can be performed using either direct extrusion or indirect extrusion. Direct extrusion is the most common method for producing aluminum profiles across construction, industrial, and transportation applications.
Indirect extrusion offers more uniform material flow and improved surface quality. It is also capable of producing seamless aluminum tubes, which are widely used in applications requiring higher pressure resistance, leak-tight performance, and enhanced structural reliability.


Aluminum extrusion is highly sensitive to alloy extrudability and heat-treatment response. The industry standard is the 6xxx series. Beyond 6xxx, the following series can also be extruded.
- 6xxx series (e.g., 6005, 6060, 6061, 6063, 6082; Al-Mg-Si): Excellent extrudability, wide processing window, and strong heat-treatment response to T5/T6. Balances strength, toughness, surface finish (good anodizing quality), and cost; ideal for high-volume profiles.
- 7xxx (e.g., 7003/7005/7075): High-strength; more challenging to extrude. Suited for structural parts and seamless tubes (often using indirect extrusion). Requires tight heat-treatment control.
- 2xxx (e.g., 2024): High-strength; lower flowability and narrower process window. Often paired with post-machining and heat treatment to meet final specs.
- 1xxx (e.g., 1050/1060/1100/1070): High electrical/thermal conductivity and corrosion resistance; excellent extrudability. Ideal for busbars, heat-dissipation profiles, and decorative applications.
- 5xxx (e.g., 5052/5083/5086): Mg-based non-heat-treatable alloys with good strength and corrosion resistance; suitable for applications requiring toughness and corrosion performance.
Magnesium Can Also Be Extruded Also
Compared with aluminum extrusion, magnesium extrusion offers a lighter weight advantage but demands tighter process control: it operates within a narrower temperature window, has higher sensitivity to oxidation and flow stability, and imposes stricter requirements on equipment, tooling, and safety measures.


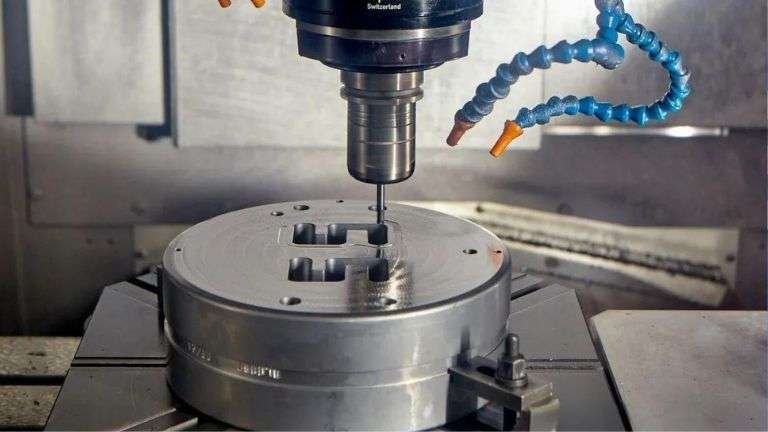
Extrusion dies are critical tools that determine the shape, dimensional accuracy, and surface quality of aluminum profiles. Well-designed dies help ensure stable metal flow, consistent tolerances, and efficient mass production.
At HTS-ALU, all extrusion dies are developed in-house based on customer drawings, CAD files, or physical samples. Our engineering team optimizes profile structures and extrusion feasibility before tooling production to improve manufacturing efficiency and product quality.
With an in-house tooling workshop, we can typically complete custom die development and sample production within 7 days, helping customers accelerate product validation and project timelines.

Aluminum extrusion on the press converts preheated billets into continuous profiles by forcing metal through a precision die under high pressure. The press capacity is expressed in tons (tonnage): larger or thicker profiles require higher-tonnage presses to provide sufficient extrusion force and maintain stable flow and dimensions.
Die and billet preheating: Preheat the die set, backer, bolster, and container to stabilize dimensions and promote uniform metal flow. Bring billets to the target extrusion temperature to achieve plasticity without incipient melting, reducing flow marks and startup defects.
Billet loading and upset: Load the heated billet into the container and perform an upset to ensure full contact, purge surface oxides, and seal against backflow. Proper upsetting minimizes lap, pick‑up, and seam defects at the extrusion start.
Ram extrusion through the die: Drive the billet through the die orifice—flat dies for solid profiles, porthole/bridge dies with mandrels for hollows—while controlling ram speed and metal exit temperature. Balance flow via bearing lengths and port design to maintain dimensional accuracy, surface finish, and weld‑line strength.
Runout and in‑line cooling (on press): Support the emerging profile on the runout table with pullers to prevent sagging and chatter.


After extrusion and cooling, aluminum profiles are straightened to remove bow, twist, and residual stress generated during the extrusion process. This step helps ensure the profile maintains the required shape and dimensional accuracy.
Straightening is typically performed by controlled stretching or leveling, depending on the profile geometry and application requirements. Proper straightening improves flatness, assembly fit, and overall product consistency before further processing.
As an important step between extrusion and heat treatment, straightening helps achieve tighter tolerances and more stable mechanical performance in the finished aluminum profile.

Heat treatment plays a key role in achieving the required mechanical properties of extruded aluminum profiles. Different cooling and aging processes are used depending on the target alloy and temper designation.
For T5 profiles, cooling is typically achieved through air or mist quenching before artificial aging. For T6 profiles, water quenching is commonly applied to maximize strength and hardness.
After quenching, the profiles undergo artificial aging under controlled temperature conditions to achieve the specified temper, ensuring consistent strength, dimensional stability, and long-term performance.