
Aluminium Properties
Aluminum is the third most abundant element in the Earth’s crust and the most widely used metal after steel. Its unique combination of properties has made aluminum indispensable across a broad range of applications, from everyday household items and industrial manufacturing to aerospace, defense, packaging, and construction materials. This article provides an overview of the key properties of aluminum that underpin its versatility and widespread use in modern society.
Physical Properties of Aluminum
Aluminum is a lightweight, silver-white metal known for its good ductility, as well as excellent electrical and thermal conductivity.
Aluminum Appearance
Aluminum has a silver-white color and metallic luster. After oxidation in air, it remains silver-white with a slightly matte texture. Most everyday aluminum products are surface treated, such as by anodizing or electrophoresis, to achieve various colors and metallic finishes.appearance.

Aluminum Molar Mass
Aluminum is the 13th element in the periodic table, containing 13 protons in its nucleus. It occurs in nature almost exclusively as the isotope ²⁷Al, with the presence of other isotopes such as ²⁶Al and ²⁸Al being negligible. The molar mass of aluminum is 26.98 g/mol.
Aluminum Density
The density of pure aluminum is 2.70 g/cm³. Most aluminum used in practical applications is in the form of alloys, and the density varies slightly depending on the alloying elements. The table below shows the densities of several common aluminum alloy grades:
| Alloy Grade | Main Alloying Elements | Density (g/cm³) |
|---|---|---|
| 1050 | Commercially pure Al | 2.71 |
| 1100 | Al, small amount of Cu | 2.72 |
| 2024 | Al-Cu-Mg | 2.78 |
| 3003 | Al-Mn | 2.73 |
| 5052 | Al-Mg | 2.68 |
| 6061 | Al-Mg-Si | 2.70 |
| 6063 | Al-Mg-Si | 2.69 |
| 7075 | Al-Zn-Mg-Cu | 2.81 |
Aluminum Melting Point
Pure aluminum has a melting point of 660.3°C (1,220.5°F) and a boiling point of 2,470°C (4,478°F). Compared to many other metals, aluminum’s melting point is relatively low. As a result, aluminum manufacturing requires less energy, and recycling processes are also more efficient. However, this low melting point makes aluminum unsuitable for high-temperature applications such as fire doors. Notably, while aluminum itself has a low melting point, its oxide, alumina (Al₂O₃), has an extremely high melting point of approximately 2,072°C (3,762°F).
For aluminum alloys, melting points can vary slightly depending on the composition of the alloy. The melting points of aluminum alloys are given as a range because the various alloying elements in the material begin to melt at different temperatures. The table below shows the melting points of several common aluminum alloy grades:
| Alloy Grade | Main Alloying Elements | Melting Point (°C) |
|---|---|---|
| 1050 | Commercially pure Al | 643–657 |
| 1100 | Al, small amount of Cu | 643–657 |
| 2024 | Al-Cu-Mg | 500–638 |
| 3003 | Al-Mn | 643–655 |
| 5052 | Al-Mg | 607–650 |
| 6061 | Al-Mg-Si | 582–652 |
| 6063 | Al-Mg-Si | 615–655 |
| 7075 | Al-Zn-Mg-Cu | 477–635 |
Aluminum Electrical Conductivity
Pure aluminum is known for its excellent electrical conductivity, which is typically around 36.9–37.7 megasiemens per meter (MS/m) at 20°C (68°F). This is approximately 61% of the International Annealed Copper Standard (IACS), making pure aluminum one of the most widely used conductive non-ferrous metals in electrical applications.
For most aluminum alloys, electrical conductivity decreases with the addition of alloying elements. However, alloys such as 6101 are designed for good conductivity and are commonly used in bus tubes for power distribution. It is also important to note that aluminum oxide (Al₂O₃), which forms on the surface of aluminum, is non-conductive and acts as an electrical insulator.
The table below presents the electrical conductivity values for several common aluminum alloy grades:
| Alloy Grade | Main Alloying Elements | Electrical Conductivity (% IACS) |
|---|---|---|
| 1050 | Commercially pure Al | 59–62 |
| 1100 | Al, small amount of Cu | 59 |
| 2024 | Al-Cu-Mg | 30 |
| 3003 | Al-Mn | 40 |
| 5052 | Al-Mg | 35 |
| 6061 | Al-Mg-Si | 43 |
| 6063 | Al-Mg-Si | 53 |
| 6101 | Al-Mg-Si | 56–59 |
| 7075 | Al-Zn-Mg-Cu | 33 |
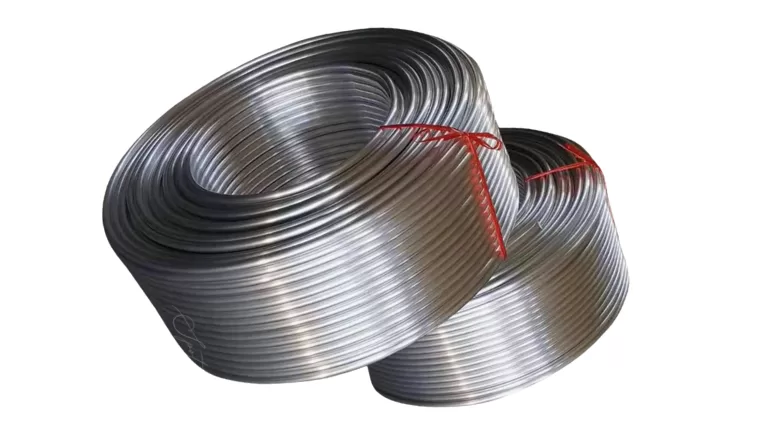
Aluminum is well known for its outstanding thermal conductivity, making it a preferred material for heat sinks and enclosures in electromechanical products. The thermal conductivity of pure aluminum is typically 235 W/m·K at room temperature. For aluminum alloys, as shown in the table below.
| Alloy Grade | Main Alloying Elements | Thermal Conductivity (W/m·K) |
|---|---|---|
| 1050 | Commercially pure Al | 222–235 |
| 1100 | Al, small amount of Cu | 220 |
| 2024 | Al-Cu-Mg | 120–130 |
| 3003 | Al-Mn | 160–170 |
| 5052 | Al-Mg | 138 |
| 6061 | Al-Mg-Si | 166 |
| 6063 | Al-Mg-Si | 201 |
| 7075 | Al-Zn-Mg-Cu | 130–150 |
Aluminum Ductility
Aluminum and its alloys exhibit excellent ductility, which is the ability to undergo significant plastic deformation prior to fracture. This property is a critical factor in their widespread use for processing and forming applications, such as aluminum foil production, extrusion, cold drawing, and rolling.
Ductility is influenced by alloying elements, heat treatment, and cold working. Copper, zinc, and silicon reduce ductility, while magnesium increases it. Heat treatment can change the ductility of an alloy, and the O (annealed) condition provides the best ductility. Cold working usually makes aluminum stronger but less ductile.
The table below shows the typical elongation values (an indicator of ductility) for several commonly used aluminum alloys:
| Alloy Grade | Series | Condition | Elongation (%) |
|---|---|---|---|
| 1050/1060 | 1xxx | O (Annealed) | 35–50 |
| 3003 | 3xxx | O | 25–30 |
| 5052 | 5xxx | O | 20–25 |
| 6061 | 6xxx | T6 | 10–15 |
| 6063 | 6xxx | T5 | 8–12 |
| 2024 | 2xxx | T3 | 10–12 |
| 7075 | 7xxx | T6 | 5–10 |
Aluminum Hardness and Wear Resistance
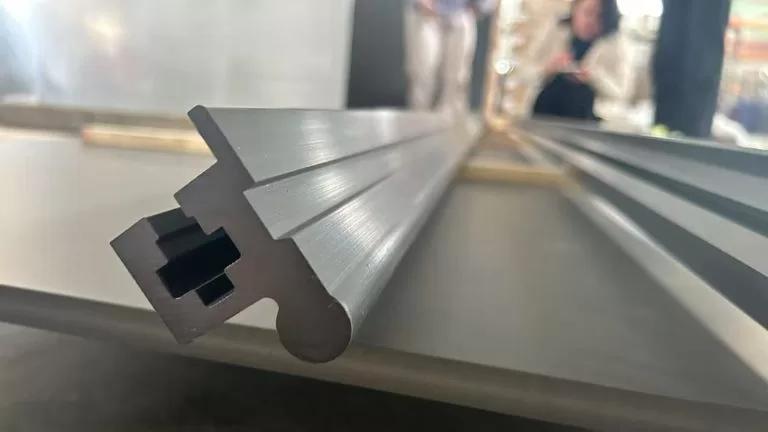
Pure aluminum is a relatively soft metal, with a typical Vickers Hardness (HV) of about 20–30 HV (equivalent to around 15 HBW on the Brinell scale). To improve the hardness and wear resistance of aluminum, several methods are commonly employed:
Alloying
The addition of elements such as copper, magnesium, silicon, and zinc can significantly increase the hardness and wear resistance of aluminum materials. For example:
- 2024 aluminum alloy (main alloying element: copper) can reach a hardness of 120–140 HV after T6 heat treatment.
- 6061 aluminum alloy (main alloying elements: magnesium and silicon) has a hardness of approximately 95 HV in the T6 condition.
- 7075 aluminum alloy (main alloying elements: zinc and magnesium) can achieve a hardness of 150–170 HV after T6 treatment.
Heat Treatment
Various heat treatment conditions, such as T6 (solution treatment followed by artificial aging), can further enhance the hardness of these alloys.
Anodizing
Anodic oxidation treatment of the aluminum surface produces a dense aluminum oxide (Al₂O₃) protective layer, which is extremely hard and offers excellent wear resistance:
- The hardness of a standard anodized layer can reach 200–300 HV.
- Hard anodizing results in a thicker oxide layer, with hardness values between 400–600 HV. Some advanced processes can achieve hardness levels exceeding 1000 HV.
Aluminum Magnetic
Aluminum is a non-magnetic metal with a magnetic susceptibility of −16.6 × 10⁻⁶, where the negative value indicates that it is diamagnetic. This means aluminum is not attracted to magnetic fields. When ferromagnetic elements such as iron (Fe) or nickel (Ni) are added, it is possible to produce aluminum alloys with weak magnetic properties; however, their magnetism remains significantly lower than that of steel.
Because of its lack of magnetism, aluminum is widely used in applications where magnetic interference must be avoided, such as in electronic enclosures and MRI equipment.
Aluminum Reflectivity
Aluminum exhibits excellent reflectivity properties across a wide range of the electromagnetic spectrum.
Visible Light (380–750 nm):
A pure, non-oxidized aluminum surface has a reflectivity as high as 90%–95%, which is comparable to that of silver. After a natural oxide layer forms, the reflectivity decreases slightly to about 80%–85%.
Infrared Light (750 nm–1 mm):
In the infrared range, aluminum’s reflectivity remains high, typically between 90% and 98%. This makes aluminum an ideal material for infrared reflection applications.
Ultraviolet Light (100–380 nm):
For ultraviolet light, the reflectivity of aluminum is relatively lower, approximately 50%–70%. Despite this reduction, it still outperforms most other metals in this range.
Because of its excellent reflectivity, aluminum is commonly used in lighting fixtures, optical reflectors, solar energy devices, and thermal insulation materials.

Chemical Properties of Aluminum
Aluminum (Al) is an active, lightweight metal known for its rich and distinctive chemical behavior. Its atomic number is 13, with an electron configuration of [Ne] 3s² 3p¹. Aluminum commonly exhibits a +3 oxidation state, which is its only stable valence. The electronegativity of aluminum is 1.61 (Pauling scale), reflecting its pronounced metallic character.
Reaction with Oxygen
When exposed to air, aluminum rapidly reacts with oxygen, forming a thin, dense aluminum oxide (Al₂O₃) film on its surface. This oxide layer, usually about 4–5 nm thick, serves as a protective barrier and prevents further oxidation of the underlying metal.
Chemical equation:
4Al + 3O₂ → 2Al₂O₃
If the temperature exceeds aluminum’s melting point (660°C) or if the protective oxide layer is disrupted, aluminum can react vigorously with oxygen, resulting in intense combustion and the release of significant heat.
Furthermore, aluminum powder or thin foil can easily ignite and undergo explosive combustion (dust explosion) if exposed to an open flame in air.
The intense combustion of aluminum has practical applications in pyrotechnics and solid rocket propellants. Aluminum powder is widely used in fireworks, flares, and solid rocket fuels to provide bright illumination and increase thrust output.
Thermite Reaction of Aluminum
The thermite reaction involves mixing aluminum powder with metal oxides such as iron(III) oxide (Fe₂O₃) or manganese dioxide (MnO₂) and igniting the mixture. In this process, aluminum acts as a reducing agent, taking oxygen from the metal oxide and producing a large amount of heat:
2Al + Fe₂O₃ → Al₂O₃ + 2Fe (ΔH = −851.5 kJ/mol)
This reaction is utilized in applications such as thermite welding for joining railway tracks, the fabrication of military incendiary devices, and the production of high-melting-point metals such as chromium and manganese.

Reaction of Aluminum with Acids
Aluminum readily reacts with non-oxidizing acids such as hydrochloric acid and dilute sulfuric acid, producing the corresponding aluminum salt and releasing hydrogen gas (H₂).
In contrast, oxidizing acids like concentrated nitric acid and concentrated sulfuric acid cause aluminum to become passive at room temperature by forming a protective oxide layer, which prevents further reaction. However, under heated or highly concentrated conditions, aluminum can still react with these oxidizing acids.
As a result, aluminum containers should not be used to store non-oxidizing acids such as hydrochloric acid, as this can lead to corrosion and hydrogen gas evolution. Conversely, aluminum is generally safe for storing concentrated nitric acid due to the passivation effect. In industrial applications, dilute acids such as phosphoric acid are sometimes used to remove surface oxides from aluminum, but the exposure time must be carefully controlled to prevent excessive corrosion.
Reaction of Aluminum with Alkalis
Aluminum dissolves readily in alkaline solutions, forming aluminate ions (AlO₂⁻ or [Al(OH)₄]⁻) and releasing hydrogen gas (H₂). The process begins with the dissolution of the protective aluminum oxide (Al₂O₃) film on the metal’s surface. This oxide reacts with sodium hydroxide to produce sodium aluminate and water:
Al₂O₃ + 2NaOH → 2NaAlO₂ + H₂O
Once the oxide layer is removed, the exposed aluminum metal reacts with water, generating aluminum hydroxide and hydrogen gas:
2Al + 6H₂O → 2Al(OH)₃ + 3H₂↑
The aluminum hydroxide formed can further react with sodium hydroxide to yield soluble sodium aluminate:
Al(OH)₃ + NaOH → Na[Al(OH)₄]
This strong reactivity with alkalis is utilized industrially, for example, to remove grease and oxide layers from aluminum surfaces using dilute sodium hydroxide solutions. However, exposure time must be carefully controlled to prevent excessive corrosion.
Reactions of Aluminum with Other Metals
When aluminum (anode) is electrically coupled with a more noble metal such as copper (cathode), electrochemical corrosion occurs. The half-reactions are as follows:
Anodic reaction (aluminum):
Al → Al³⁺ + 3e⁻
Cathodic reaction (neutral or alkaline medium):
O₂ + 2H₂O + 4e⁻ → 4OH⁻
As a result, the aluminum surface develops pits (localized corrosion), while white aluminum hydroxide (Al(OH)₃) deposits are typically seen near the copper. A similar process occurs when aluminum is in contact with stainless steel; therefore, electrical insulation between these metals is necessary to prevent galvanic corrosion.
Reaction with Mercury
When aluminum comes into contact with mercury, an aluminum-mercury amalgam (Al-Hg alloy) forms. This process breaks down the protective oxide layer on aluminum, allowing rapid corrosion. Water then reacts with the exposed aluminum to produce aluminum hydroxide and hydrogen gas:
2Al + 6H₂O → 2Al(OH)₃ + 3H₂↑
Because of its destructive effect on aluminum, mercury is strictly prohibited on aircraft to ensure the integrity and safety of aluminum components.

Aluminum Is Non-Toxic
Aluminum is considered non-toxic and chemically stable under most conditions, making it suitable for use in products that come into contact with food and beverages. As a result, it is commonly utilized in the manufacture of cans, utensils, and food packaging materials.
Protective Coating in Beverage Cans
To prevent any potential reaction between the aluminum can and acidic or carbonated beverages, a protective coating is applied to the inner surface of aluminum cans. This coating serves as a barrier, ensuring that the contents remain uncontaminated while preserving the can’s structural integrity and the beverage’s quality.
Aluminum Mechanical Properties
Pure Aluminum Mechanical Properties
Pure aluminum is characterized by relatively low strength but exhibits excellent ductility and electrical conductivity. These properties make it suitable for applications that prioritize malleability and electrical or thermal performance over mechanical strength.
Typical values for annealed pure aluminum include:
- Tensile Strength: 70–100 MPa
- Yield Strength: 20–50 MPa
- Elongation: 30–50%
- Brinell Hardness (HB): 15–25
- Young’s Modulus: 69 GPa
Mechanical Properties of Aluminum Alloys
The mechanical properties of aluminum alloys vary widely depending on their composition and temper (heat treatment or work hardening). The following table summarizes typical mechanical properties for several representative aluminum alloys:
| Alloy | Temper | Tensile Strength (MPa) | Yield Strength (MPa) | Elongation (%) | Hardness (HB) |
|---|---|---|---|---|---|
| 1050 | O | 70–100 | 20–50 | 30–50 | 15–25 |
| 1050 | H18 | 150 | 140 | 5 | 35 |
| 2024 | T3 | 470 | 325 | 10 | 120 |
| 2014 | T6 | 480 | 415 | 8 | 135 |
| 5052 | H32 | 210 | 160 | 12 | 60 |
| 5083 | H116 | 290 | 215 | 12 | 80 |
| 6061 | T6 | 310 | 275 | 12 | 95 |
| 6063 | T5 | 190 | 160 | 12 | 60 |
| 7075 | T6 | 570 | 505 | 11 | 150 |
| 7050 | T74 | 520 | 455 | 10 | 140 |
| A356 | T6 | 260 | 200 | 6 | 80 |
Aluminum Fatigue Resistance
Aluminum possesses moderate fatigue strength, which means it can withstand repeated cyclic loading reasonably well compared to many other metals. This property, along with its low density, makes aluminum and its alloys ideal choices for automotive and aerospace applications where weight savings and resistance to fatigue failure are critical requirements. Shot peening is often used to improve the fatigue resistance of aluminum by introducing beneficial compressive stresses on its surface.
Aluminum Low-Temperature Strength
Most aluminum alloys become stronger as the temperature decreases, with both yield and tensile strength increasing. Unlike steel, aluminum retains good toughness at low temperatures and does not become brittle. However, some high-zinc 7xxx series alloys, such as 7075, may show slight embrittlement under extremely low temperatures.
Aluminum Coefficient of Thermal Expansion
Aluminum has a linear coefficient of thermal expansion of about 23.1 × 10⁻⁶ /°C. Pure aluminum’s coefficient of thermal expansion is high compared to many other metals, and it is close to that of other light metals like magnesium but much higher than that of steel (about 12 × 10⁻⁶ /°C). While the addition of alloying elements in aluminum alloys can result in minor changes, the thermal expansion coefficient remains relatively consistent.
Machinability of Aluminum
Aluminum has excellent machinability and can be processed into various shapes and sizes through extrusion, rolling, drawing, and stamping. It also performs well in cutting, welding, and brazing operations, with low energy consumption and high efficiency, making it highly suitable for industrial production and manufacturing of complex components.

Aluminum Machinability
Pure aluminum and most aluminum alloys generally exhibit good machining performance, characterized by low cutting resistance, easy chip breaking, and extended tool life. In contrast, high-silicon aluminum alloys and some high-strength alloys have higher hardness, which can accelerate tool wear and therefore require the selection of appropriate cutting tools.
Additionally, softer aluminum alloys may tend to stick to cutting tools during machining, a problem that can be alleviated by using cutting fluids or harder tool materials.
Aluminum Casting Performance
Aluminum has a low melting point (660°C), which reduces energy consumption during melting and allows for efficient processing. Its excellent fluidity enables the production of highly intricate castings. The solidification shrinkage rate of aluminum alloys is about 6%, so proper feeding system design is essential to ensure high-quality castings. Aluminum also tends to absorb hydrogen, which can lead to gas porosity; therefore, melt refining techniques such as argon degassing are often used.
Aluminum Die Casting
Aluminum is also well-suited for die casting, a process that uses reusable metal molds and rapid cooling to achieve multiple production cycles per minute. As a result, die casting delivers much higher production efficiency than traditional casting methods.
Aluminum Welding Performance
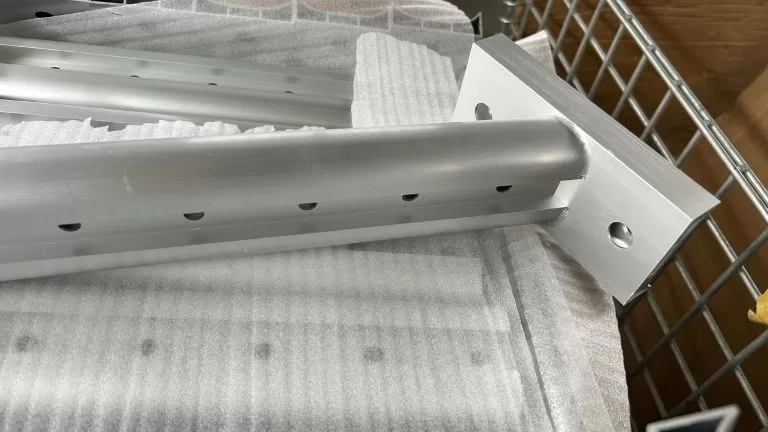
Aluminum’s thermal conductivity is about three times higher than that of steel. As a result, more heat input is required during welding—processes like TIG or MIG welding often need higher current or preheating. Although aluminum itself melts at a relatively low temperature (660°C), its surface oxide layer (Al₂O₃) melts at a much higher temperature (2050°C). This makes the oxide layer difficult to remove, so surface cleaning or the use of AC-TIG welding (which provides a cathodic cleaning effect) is necessary. Additionally, aluminum has a high coefficient of thermal expansion, which can cause significant welding distortion. To control deformation, proper fixturing or segmented welding techniques are recommended.
Aluminum Rolling Performance
Aluminum possesses excellent ductility, making it highly suitable for rolling processes. For example, 1xxx series aluminum can be rolled into extremely thin foil, reaching thicknesses as low as 0.0005 mm. The 3xxx series is commonly used for rolling applications such as beverage can bodies, due to its good formability and mechanical performance. The 6xxx series alloys are well-suited to hot rolling, as they exhibit favorable plasticity at temperatures above 400°C, making them ideal for the production of thick plates.
Aluminum Sheet Metal Forming Performance
Aluminum sheet is well-suited for various cutting methods, including laser cutting, waterjet cutting, and punching. Its excellent ductility enables precise and efficient fabrication.
For bending, the minimum bend radius depends on both alloy type and sheet thickness. For example, 5052-H32 aluminum typically requires a minimum bend radius of 1.5 times the material thickness. Springback is a common issue with aluminum, often addressed by over-bending the part by 5° to 10°, or by employing corrective pressing or artificial aging (as with 6061-T6).
In stamping and deep drawing, pure aluminum (1050-O) and 5xxx series alloys (such as 5083-O) provide the best formability, with limit drawing ratios (LDR) up to 2.0. High-strength aluminum alloys (e.g., 2024-T3) are generally formed at elevated temperatures (200–300°C) to improve performance. To prevent sticking and damage, molds are often optimized using polyurethane or chrome plating. Appropriate lubricants, such as mineral oil or polyvinyl alcohol (PVA), are used to reduce friction and ensure good surface quality.
Aluminum in Cold Drawing/Cold Working Performance
Aluminum is well-suited for cold drawing or cold working processes when producing high-precision and small-sized products. However, it is important to control work hardening and springback during processing. 1xxx, 3xxx, and 5xxx series aluminum alloys are preferred for cold drawing, while high-strength alloys such as the 7xxx series are generally not recommended for direct cold forming.
Aluminum Extrusion Performance
Aluminum and its alloys have excellent extrudability. Thanks to their good plasticity and strong flowability, aluminum materials can be extruded into various complex profiles and tubes at relatively low temperatures and pressures. The extrusion process offers high production efficiency and enables the manufacture of thin-walled, intricate, and long-length products with high dimensional accuracy.
The 1xxx, 3xxx, and 6xxx series aluminum alloys are especially suitable for extrusion, while some high-strength alloys (such as the 2xxx and 7xxx series) are more difficult to extrude. Aluminum extrusion is widely used in architectural profiles, transportation, electronics, and many other fields.

Other Processing Methods for Aluminum
Aluminum Honeycomb: Aluminum honeycomb panels provide exceptional strength-to-weight ratio and are widely used in aerospace and construction for lightweight structural applications.
Foamed Aluminum: Foamed aluminum features a porous structure, offering excellent energy absorption and sound insulation properties for automotive and architectural uses.
3D Printing: Aluminum alloys can be processed through additive manufacturing, enabling the production of complex geometries and customized components with high precision.
Superplastic Forming: Certain aluminum alloys demonstrate superplasticity at elevated temperatures, allowing the creation of intricate, thin-walled shapes through superplastic forming processes.
Microporous and Porous Aluminum: Microporous and porous aluminum materials are engineered with controlled porosity for applications such as filtration, fluid diffusion, and lightweight structures.